OEE Summary
**In short:** OEE multiplies Availability, Performance, and Quality into one score for how productively your equipment runs. Mantsu feeds all three factors automatically from registered downtimes, confirmations, and scrap.
Overall Equipment Effectiveness (OEE) is the manufacturing industry standard for measuring how productively a machine or production line is being used. An OEE score of 100% means you are producing only good parts, as fast as possible, with no unplanned stops.
OEE is not a single number. It is the product of three factors, each measuring a different type of loss:
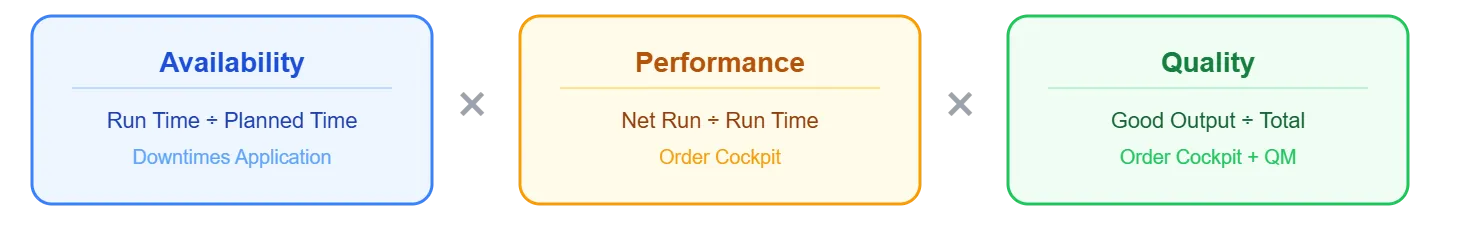
Mantsu captures all the data needed to calculate OEE directly from operator interactions on the shop floor.
The Time Model
To understand OEE, it helps to think in terms of time. Every loss "eats into" the available production time, layer by layer:
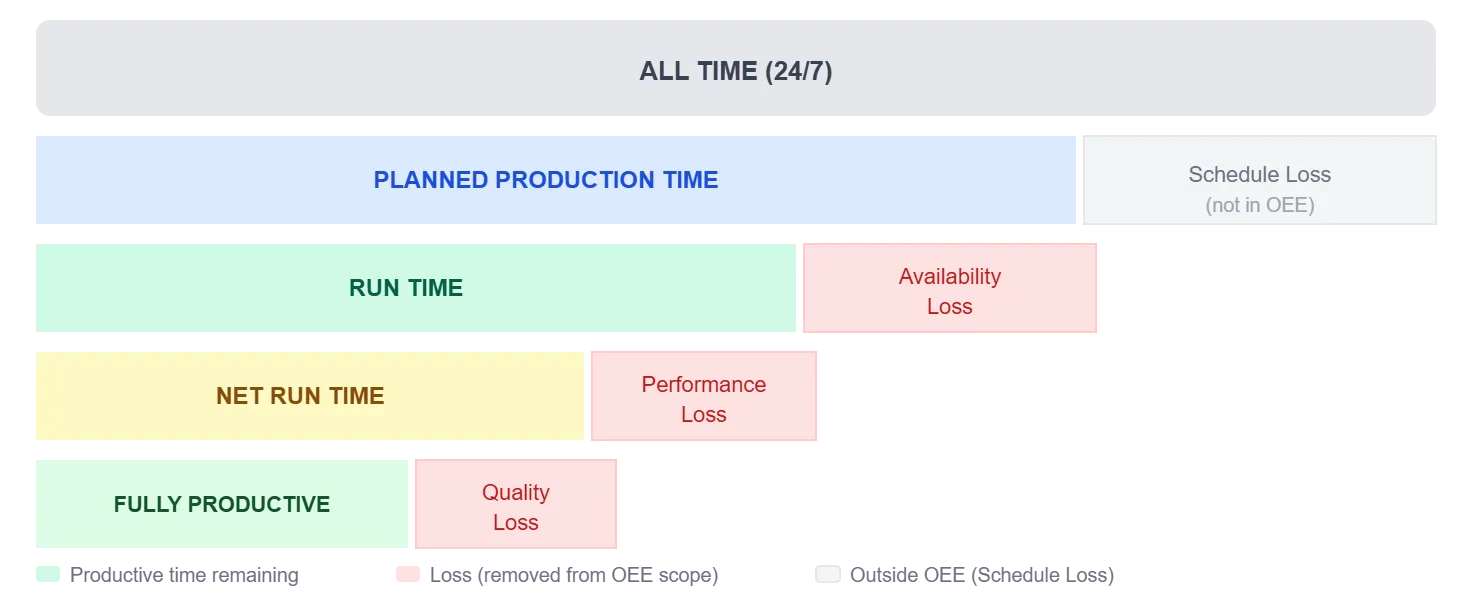
Each row shows how much productive time remains after each layer of loss is removed.
Time Block | What it represents |
|---|---|
All Time | Every minute of every day (24/7) |
Planned Prod. Time | The time your equipment is scheduled to run (shifts, calendars) |
Run Time | Planned time minus downtime events; the machine was actually running |
Net Run Time | Run time minus performance losses; the machine ran at its ideal speed |
Fully Productive Time | Net run time minus quality losses; only good parts were produced |
The goal of OEE is to maximise Fully Productive Time.
Availability
Availability measures how much of your planned production time the equipment was actually running.
Availability = Run time / Planned Production Time
Any event that stops production for a meaningful period counts as an Availability Loss:
Loss type | Examples | In Mantsu |
|---|---|---|
Unplanned stops | Machine breakdown, material shortage | Registered with a dedicated reason code in the Downtimes Manager & via the Order Cockpit for the operator |
Planned stops | Changeover, scheduled maintenance, cleaning | Scheduling |
In Mantsu, every downtime event has a start time, stop time, and reason code drawn from the configured reason tree. This makes it possible to see exactly which stop types are hurting your availability and where to focus improvement.
100% availability means no stops occurred during planned production time.
Performance
Performance measures whether the equipment ran at its maximum theoretical speed during the time it was running.
The maximum theoretical speed needs to be set correctly in master data & can vary per product, or this factor can exceed 100%, which does not provide a correct total OEE.
Performance = Net Run Time / Run Time or equivalently: Performance = Actual Output / Theoretical Output
Performance Loss captures two subtleties that are easy to miss:
Loss type | Description | In Mantsu |
|---|---|---|
Short stops | Brief interruptions too short to log as a downtime event | Automatically captured below the short stop threshold in the Downtimes Manager |
Reduced speed | Machine running, but slower than the ideal cycle time | Derived from confirmed quantities vs. the expected rate for the order |
The Order Cockpit records confirmations (actual output) against production orders that carry a planned quantity and planned time window. The gap between what was produced and what could have been produced at full speed is your Performance Loss.
100% performance means that the process ran at its theoretical maximum speed whenever it was running.
Quality
Quality measures what fraction of the output was good on the first pass: no rework, no scrap.
Quality = Good Output / Total Output
Quality Loss is straightforward but costly because you already spent availability and performance time producing parts that cannot be shipped:
Loss type | Description | In Mantsu |
|---|---|---|
Scrap | Parts that must be discarded entirely | Registered per order in the Order Cockpit with a scrap reason code |
Rework / rejects | Parts that fail inspection and need re-processing | Captured through failed inspection lots in the QM module |
Because scrap is logged with a reason code and linked to a material and order, Mantsu gives you the traceability to understand why quality losses occur, not just how many.
100% quality means every confirmed part is produced first-time right and passed inspection with no scrap and no rework.
How do you calculate OEE?
A simple example with real numbers:
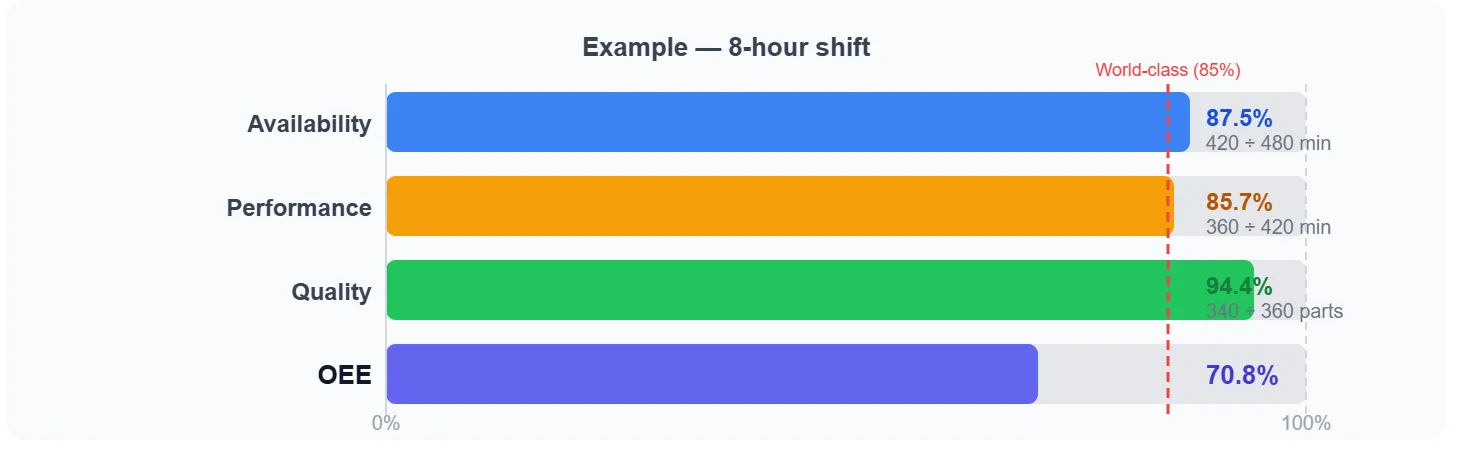
Even when each individual factor looks reasonable, the combined OEE reveals a significant amount of lost capacity.
World-class OEE is generally considered to be around 85%. Most manufacturing operations start between 40% and 60%, which highlights how much untapped capacity typically exists.
How does Mantsu support OEE?
Mantsu does not calculate OEE automatically out of the box, but it captures all the raw data needed to do so:
OEE Factor | Data source in Mantsu |
|---|---|
Availability | Downtime events with reason codes (Downtimes Manager) |
Performance | Confirmed quantities vs. planned quantities per order (Order Cockpit) |
Quality | Scrap registrations with reason codes + inspection results (Order Cockpit + QM) |
Planned time | Shift and calendar definitions (Core: Shift & Calendar Management) |
This data can be exposed through the Insights module or via an external reporting layer to calculate and visualize OEE per equipment, shift, or time period.
Why does OEE matter?
OEE turns shop floor activity into a single, comparable score. More importantly, the three underlying factors tell you where your losses are coming from:
- A low Availability score points to your Downtimes Manager data: which reason codes appear most?
- A low Performance score points to short stops and speed losses: are operators clearing micro-jams that never get logged?
- A low Quality score points to scrap and inspection data: which materials or operations produce the most rejects?
By connecting OEE analysis to the structured, operator-captured data in Mantsu, you move from a lagging indicator to an actionable improvement loop.
Frequently asked questions
What is a good OEE score? An OEE of around 85% is commonly cited as world class for discrete manufacturing, but the most valuable use of OEE is tracking your own trend over time and comparing like with like.
Where does Mantsu get the OEE data? From normal operator interactions: downtime registrations feed Availability, confirmations and machine counters feed Performance, and scrap registrations feed Quality. No separate data entry is needed.
What is the difference between a downtime loss and a performance loss? A downtime loss is a registered stop with a reason code. A performance loss is time lost while the machine keeps running, such as reduced speed or short stops below the threshold.